Diamond Grit For Saw Blades And Core Drills
What This Process Needs To Solve
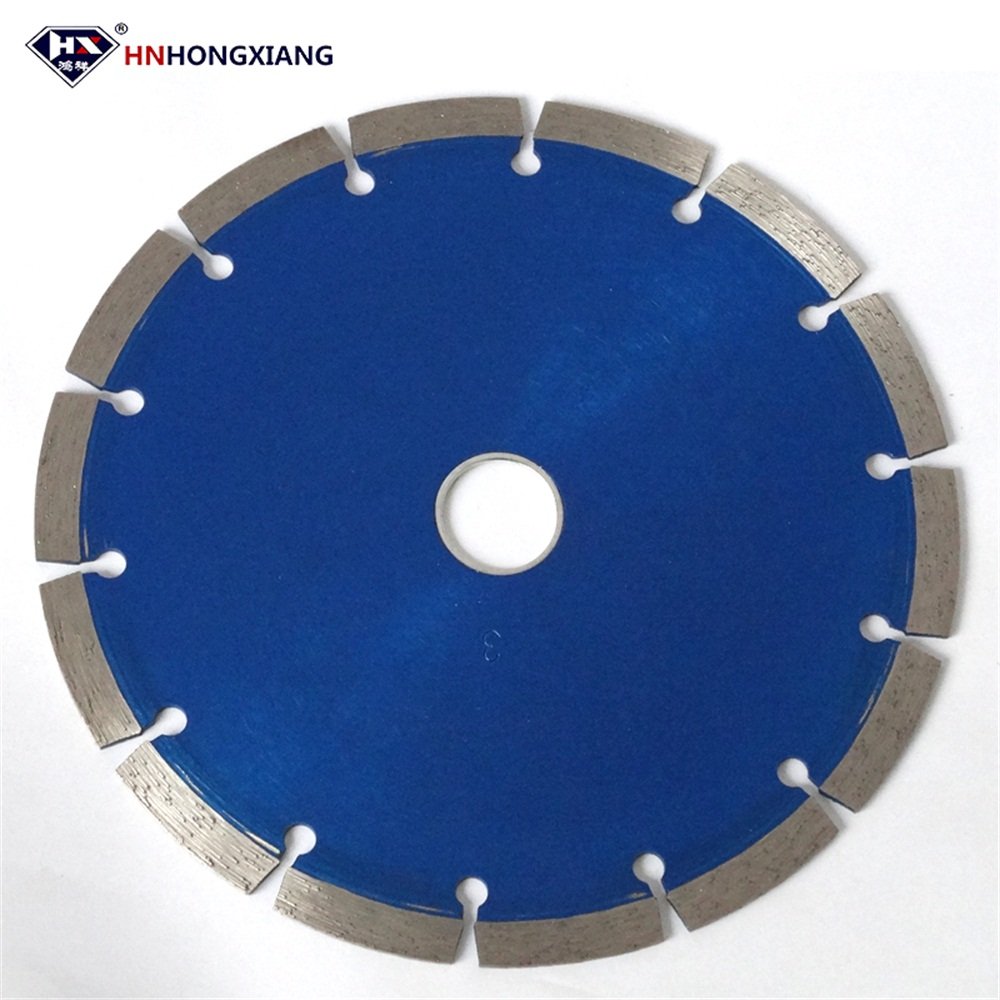
This is the raw material side of tool making. Saw blade segments, core drills and electroplated tools all work by holding diamond grit in a metal or nickel matrix, and the grit specification decides whether the tool cuts freely and wears out evenly, or glazes over on the first slab. We supply the grit for all three tool families.
Sintered saw segments run on 30/35 to 50/60 mesh. Core drills use 30/35 mesh for concrete and geological work, and 60# to 325# for glass and tile. Electroplated tools run 80# to 400#, with dental burs usually sitting between 100# and 325#.
Why strength, not size, decides segment life
A segment on a granite saw takes impact loading on every revolution. Grit that fractures on the first pass is gone, and what the bond is left holding is a ring of broken particles with no cutting edges, which is how a segment glazes. The MBD series is selected for exactly this: measurable impact strength, a regular crystal shape, and the thermal stability to survive a sinter. Titanium coating is available where the customer wants a stronger bond between grit and matrix, and it also helps on segments run without coolant.
Electroplated tools: purity and demagnetisation
On an electroplated tool the diamond sits in a nickel layer a few tens of microns thick, so the coating has to grip every single particle. That makes purity and surface condition the critical variables rather than size. We supply high-purity, demagnetised grit so the plating bath does not pull the particles into clusters before they reach the tool.
Recommended Grit By Tool Type
Grit is quoted against the tool the customer makes, because impact strength, coating and purity matter in different proportions for each family.
| Tool | Recommended grade | Grit / mesh | Why this grade |
|---|---|---|---|
| Metal bond saw blades and segmentsGranite, marble, reinforced concrete, quarry blocks | |||
| Granite and marble segments | MBD series, Ti-coated available | 30/35, 35/40, 40/45 mesh | High impact strength for sintered segments |
| Reinforced concrete and quarry | MBD heavy grade, Ti-coated | 40/45, 45/50, 50/60 mesh | Coarser grit resists impact loading |
| Core drillsGeological exploration, glass, tile, stone, concrete coring | |||
| Concrete and geological coring | MBD-12 / SMD25 / SMD30 | 30/35 mesh | Impact resistance and wear life |
| Glass and tile drills | MBD / MBDS | 60# – 325# | Finer grit for a clean hole edge |
| Electroplated toolsDental and nail burs, files, wheels, drills, saw blades | |||
| Dental and nail burs | MBD series, high purity | 100# – 325# | Demagnetised, plating bath stays clean |
| Files, wheels and saws | HDYR / HDHR crushed grit (RVD), MBD | 80# – 400# | Sharp blocky particles held in the nickel layer |
Coating weight is quoted against the customer plating bath. Grit is supplied demagnetised, with impact strength reported on the certificate where a sintered segment is involved.
What has to hold
- High impact strength for sintered segments
- Thermal stability through the sinter cycle
- Regular crystal shape, free of long splinters
- High purity and demagnetised for plating
Where it ships
Diamond Grades For This Process
Factory Direct Since 1990
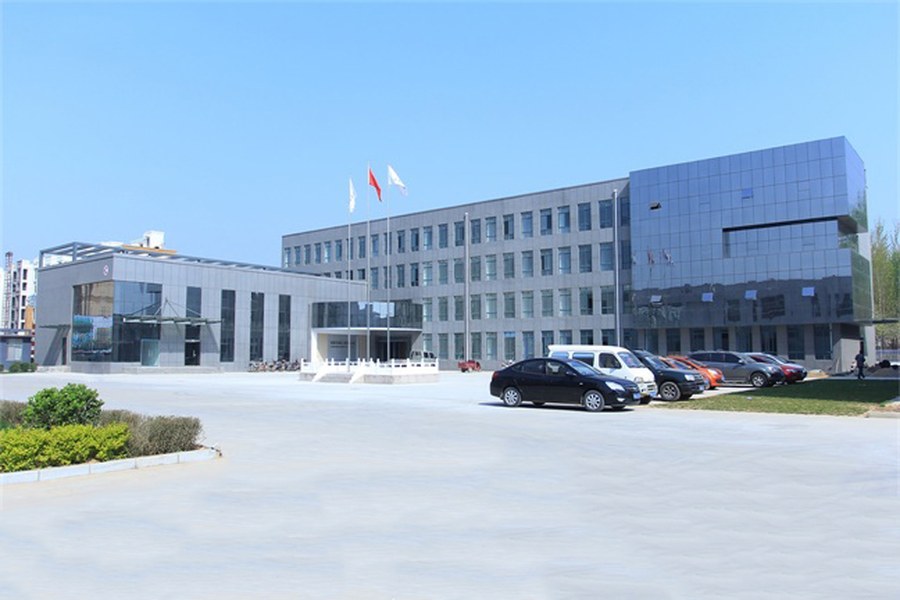
Zhecheng Hongxiang Superhard Material Co., Ltd. is an integrated manufacturer and exporter of synthetic diamond powders since 1990, located in the Diamond Capital of China.
- Own manufacturing base in Zhengzhou, Henan — powder, coating and grading on one site.
- In-house particle size and SEM inspection on every batch before packing.
- Export packing with neutral or custom label, plus sample quantities for process trials.
What To Include
Describe your workpiece, process and target result. We will match the diamond grade from the existing product range.