Functional Diamond
Functional diamond is where the diamond stops being only an abrasive. A metal coating, an agglomerated cluster or a doping element each change how the particle behaves in a bond, a slurry or a coating, and in each case the result is a property the plain material does not have.
Functional Diamond Range
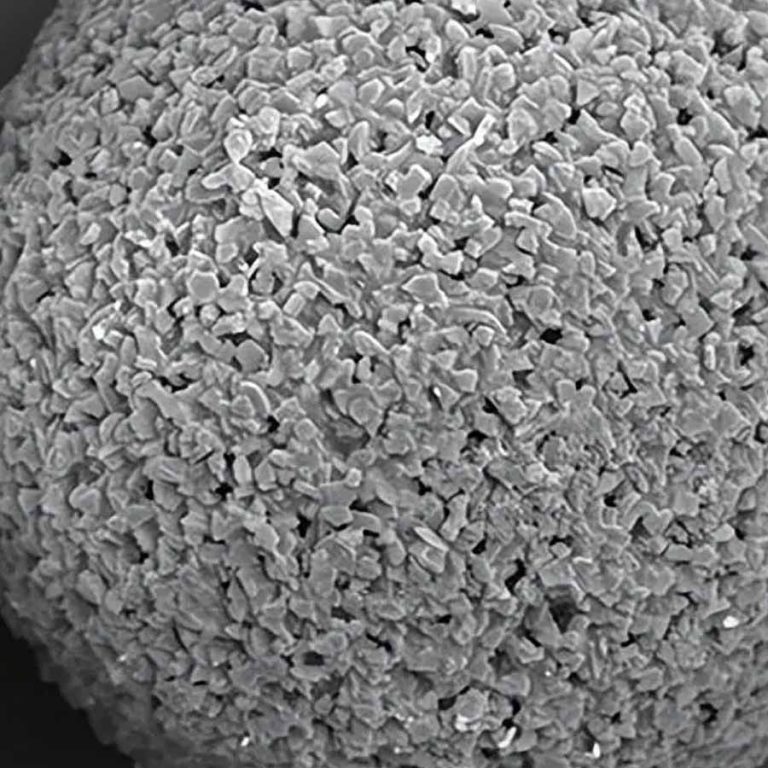
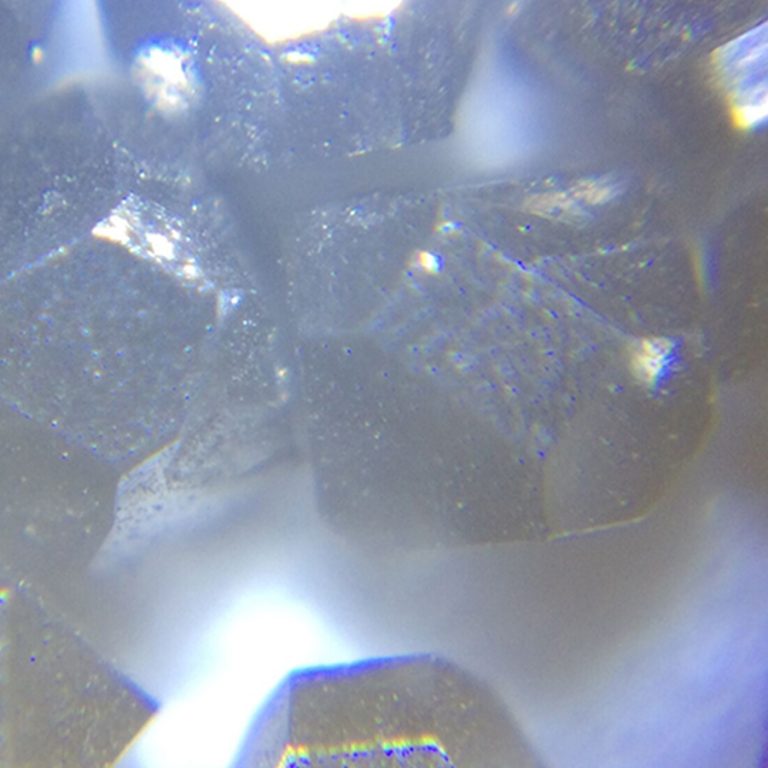
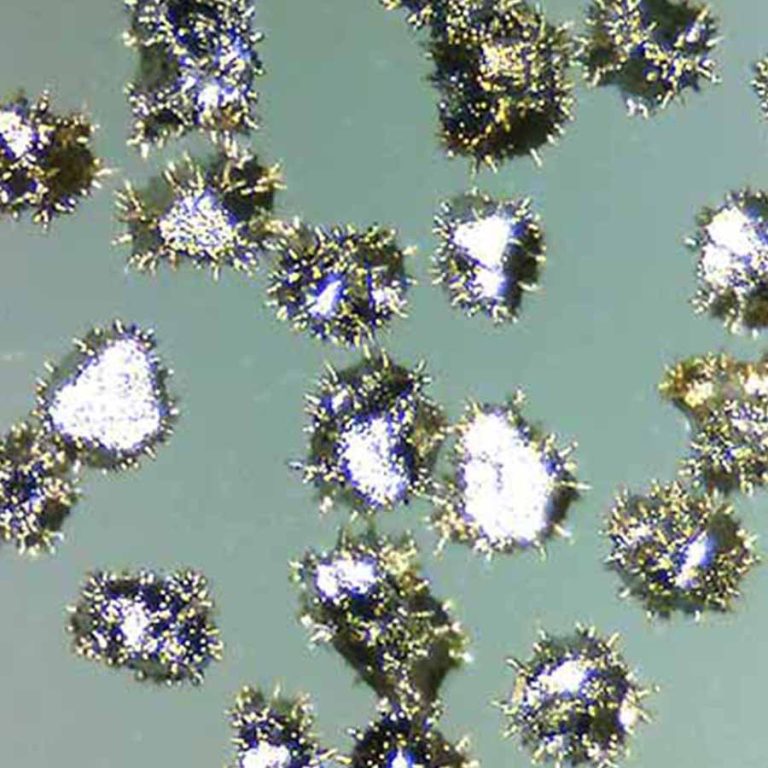
Titanium-coated diamond is there for heat: at sintering and grinding temperatures an uncoated particle oxidises and graphitises, and the titanium layer isolates it from that reaction while bonding it into the metal matrix. Nickel-coated diamond works mechanically: the rough, spiky layer keys into the bond and improves holding force, typically raising tool life by 20 to 35 percent against the same uncoated grade. Agglomerated diamond (HDYS) is micron diamond held in a near-spherical cluster that behaves as a single abrasive with many cutting edges and renews itself as it wears. Boron-doped diamond (HBDD) is a different material class altogether: boron in the diamond lattice turns an insulator into a p-type semiconductor while keeping the hardness and chemical inertness.
Which Functional Grade To Choose
| If your tool or process needs | Choose | Why |
|---|---|---|
| Diamond retention in a metal bond at sintering temperature | T (Titanium coated) | A dense titanium layer isolates the diamond from oxidation and graphitisation and reduces pull-out |
| Higher holding force in a resin or electroplated bond | N (Nickel coated) | A rough, spiky nickel layer keys mechanically into the bond; tool life typically improves 20 to 35 percent |
| Uniform coating weight across the batch | N, electroless | Electroless deposition is even in all directions rather than only where the current reaches |
| A single abrasive that renews its own cutting edges | HDYS (Agglomerated) | Near-spherical clusters act as one abrasive with many edges and reduce pad or wheel dressing |
| An electrode that will not corrode | HBDD (Boron doped) | p-type semiconducting diamond with a wide electrochemical window and low background current |
Functional Diamond Grade And Size Range
| GradeChinese standard | Size range (µm)International standard | Sieve no. / meshMesh no. | Coating route |
|---|---|---|---|
| Micron gradesW7 – W40Resin-bond wheels, diamond wire, electroplated burrs | |||
| W7 | 4–8 | 3,000 | Electroplated and electroless |
| W10 | 4–9 / 6–12 | 2,500 / 1,800 | Electroplated and electroless |
| W14 | 7–14 / 8–16 | 1,500 / 1,300 | Electroplated and electroless |
| W20 | 12–22 | 1,000 | Electroplated and electroless |
| W28 | 20–30 | 700 | Electroplated and electroless |
| W40 | 30–40 | 450 | Electroplated and electroless |
| Mesh gradesD46 – D213 (325# – 70#)Metal-bond saw segments, drills, electroplated tools | |||
| D46 | 325/400 | 325# | Electroplated and electroless |
| D54 | 270/325 | 270# | Electroplated and electroless |
| D64 | 230/270 | 230# | Electroplated and electroless |
| D76 | 200/230 | 200# | Electroplated and electroless |
| D91 | 170/200 | 170# | Electroplated and electroless |
| D107 | 140/170 | 140# | Electroplated and electroless |
| D126 | 120/140 | 120# | Electroplated and electroless |
| D151 | 100/120 | 100# | Electroplated and electroless |
| D180 | 80/100 | 80# | Electroplated and electroless |
| D213 | 70/80 | 70# | Electroplated and electroless |
Finer grades from W3 to W5 are available with electroless nickel on request. Coating weight gain, layer uniformity and the base diamond grade are confirmed against your bond system before production.
Coating Choice And What It Changes
Titanium, for temperature
Titanium coating is applied where the tool sees high temperature — metal-bond saw segments, blades and drills. The dense layer stops the diamond oxidising and graphitising during sintering and in the cut, and bonds the particle into the matrix so it is not lost as a loose inclusion.
Nickel, for holding force
Nickel coating is applied where the bond has to grip the particle. Electroplated nickel gives a deliberately rough layer that keys mechanically into the bond; electroless nickel (the N grade) deposits evenly in all directions so coating weight is more uniform. Weight gain is specified as 30 percent or 56 percent in both.
Agglomerated, for self-renewal
An agglomerate is a cluster of micron diamond in a binder, not a coated particle. It cuts at the cluster size while producing a finish closer to the size of the grains inside it, and releases dull surface grains to expose new edges underneath — which is what reduces dressing frequency.
Functional Diamond Questions
How much does nickel coating add to the particle weight?
Why coat diamond at all?
How much longer does a coated tool last?
What is the finest grade you coat?
What is boron-doped diamond used for?
What To Include
Tell us which product family you are checking and what result you need. We will recommend a specific grade and sample route.