Diamond Powder For Ceramic Squaring Wheels
What This Process Needs To Solve
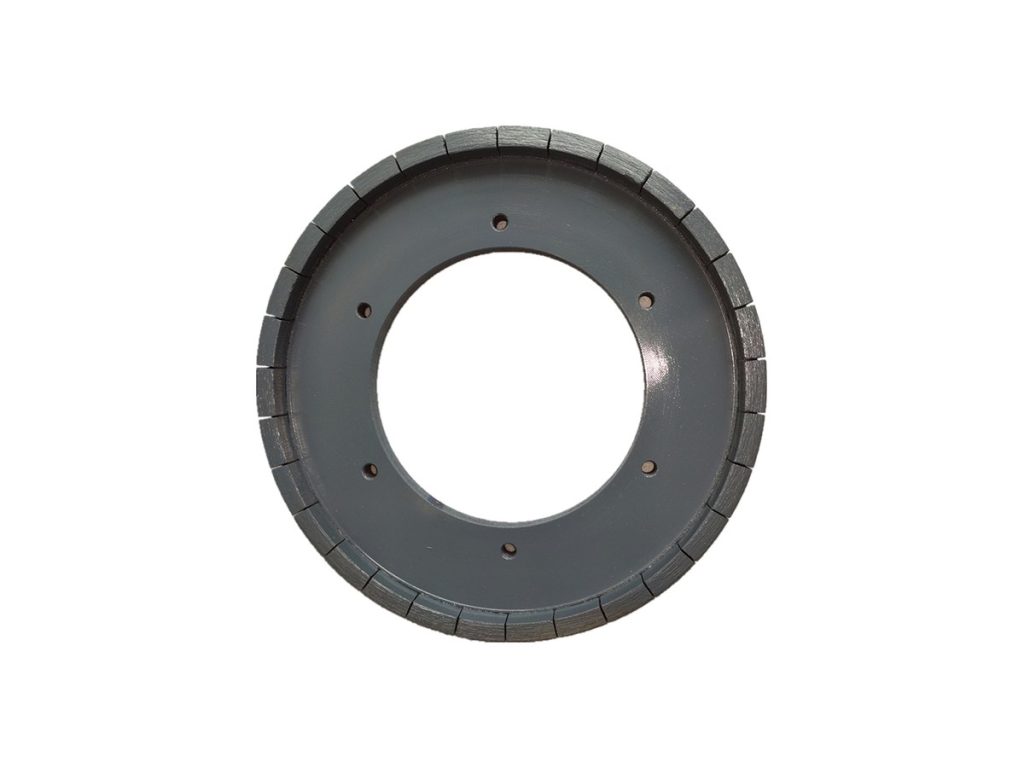
Squaring decides whether a tile leaves the line at 600.0 mm or at 599.4 mm. The wheel takes two to four millimetres off a fired edge that is harder than the bond holding the diamond, so cost is set by two numbers: how much diamond is still embedded at the end of a shift, and how many tiles were rejected for chipping. Ceramic does not behave like stone here. It fractures instead of deforming, which means one crystal above the band leaves a spall that fails the tile at inspection while the wheel itself still looks serviceable.
Why The Edge Chips Before The Wheel Wears
A chip is a particle-size problem before it is a bond problem. Resin bond squaring wheels are specified 80/100 to 325/400 mesh, and the half of that range that matters on ceramic is the top cut. A single crystal above the band scores a fracture that runs under the glaze, and there is no plastic flow afterwards to close it. Screening the coarse tail is worth more on a tile line than shifting the average size down.
The second cause is bond hardness. A bond too hard for the spindle load holds the diamond until the edges round over; the wheel then rubs rather than cuts, amp draw climbs, and the operator answers with feed pressure — which is the point where spalling begins. Self-sharpening has to be designed in, which is why HDYR and HDGR are both friable: a worn crystal fractures and exposes a fresh edge instead of glazing over.
Grade And Grit Band
Resin bond wheels run HDYR on a standard line, and HDGR where the bond is already soft and cost per wheel dominates. Metal bond squaring and cutting blades run far coarser, 30/35 to 140/170 on MBD grit, Where the stock comes off a bevel rather than the flat edge, the band is specified tighter — the chamfer and arris wheel page covers that case.
Where It Goes Wrong
- Chips on one side of the tile only. Spindle run-out or a wheel mounted off centre; true the flange before changing the band.
- Wheel glazes and amp draw climbs. Bond too hard for the grit and the load; drop one grade or raise spindle speed.
- Size drifts through the shift. Wear is not being compensated; the diamond is fine, the dress interval is not.
- Glaze lines along the edge after firing. A coarse tail in the band scoring the green body; ask for the top cut, not a finer average.
What To Put In The Enquiry
- Wheel diameter, bond type and the spindle speed it runs at.
- Grit band in mesh, plus the top cut you will accept.
- Wet or dry, and which coolant.
- Tile body, thickness and whether it is green or fired.
- Present wheel life in linear metres, so quotes are comparable.
Next Step
Send the wheel size, the bond and the chip rate you need to get under, and we will quote a screened band against it. Every batch ships with a COA carrying the PSD curve, and trial quantities are available before a production run.
Diamond Grades For Ceramic Squaring And Edge Wheels
Ceramic fractures rather than deforms, so the top cut of the band matters more than the average size. The ranges below are what ceramic lines order for squaring, chamfering and fine finishing.
| Line stage | Recommended grade | Grit band | Why this grade |
|---|---|---|---|
| Resin bond wheelsFired tile: squaring, edge grinding, lappato | |||
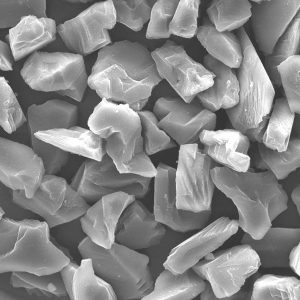
| Squaring wheel, standard line | HDYR Crushed Diamond Grit | 80/100 – 325/400 mesh | Friable crystal keeps the rim open at line speed and the cut edge chip-free |
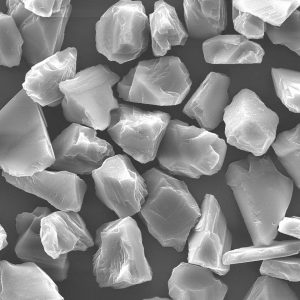
| Squaring wheel, soft bond | HDGR Crushed Diamond Grit | 100/120 – 325/400 mesh | Lower strength and faster self-sharpening where the bond is already soft |
| Chamfer and arris wheel | HDYR Crushed Diamond Grit | 140/170 – 325/400 mesh | Finer top cut on the bevel, where one pull-out reads as a glaze line |
| Lappato and fine finishing | HDG / HDY Micron Powder | W40 – W7 | Tight distribution, so gloss stays even across the tile face |
| Metal bond blades and wheelsCutting and calibration, green or fired body | |||
| Cutting and squaring blade | MBD High-Strength Diamond Grit | 30/35 – 140/170 mesh | Blocky crystal that survives the sinter cycle and the impact of a green body |
| Calibration wheel | MBD High-Strength Diamond Grit | 60/70 – 120/140 mesh | Strength held at temperature; the segment wears flat instead of shedding grit |
Grit is given in mesh here because that is how wheel drawings are specified; the micron equivalent is on each product page. A band quoted without a top cut cannot be used to predict chipping.
What has to hold
- Grit band in mesh plus the top cut you will accept
- Bond type, wheel diameter and spindle speed
- Wet or dry, and the coolant used
- Tile body, thickness and firing state
- Present wheel life in linear metres
Where it ships
Diamond Grades For This Process
Factory Direct Since 1990
Zhecheng Hongxiang Superhard Material Co., Ltd. is an integrated manufacturer and exporter of synthetic diamond powders since 1990, located in the Diamond Capital of China.
- Own manufacturing base in Zhengzhou, Henan — powder, coating and grading on one site.
- In-house particle size and SEM inspection on every batch before packing.
- Export packing with neutral or custom label, plus sample quantities for process trials.
What To Include
Describe your workpiece, process and target result. We will match the diamond grade from the existing product range.