Diamond Powder For Wear Hardfacing
What This Process Needs To Solve
Diamond survives a wear overlay only inside a time window, and every hardfacing route gives it a different one. PTA, laser cladding, oxy-acetylene spray-fusing and Ni-Cr brazing all bury diamond in metal, but they differ in how hot the pool runs and how long the particle stays in it — and that difference decides which coating and which size band you should be buying. This page is the buying side: route, grade, size band. The metallurgy behind it is in what survives the arc.
Coating Choice Follows The Route, Not The Mesh
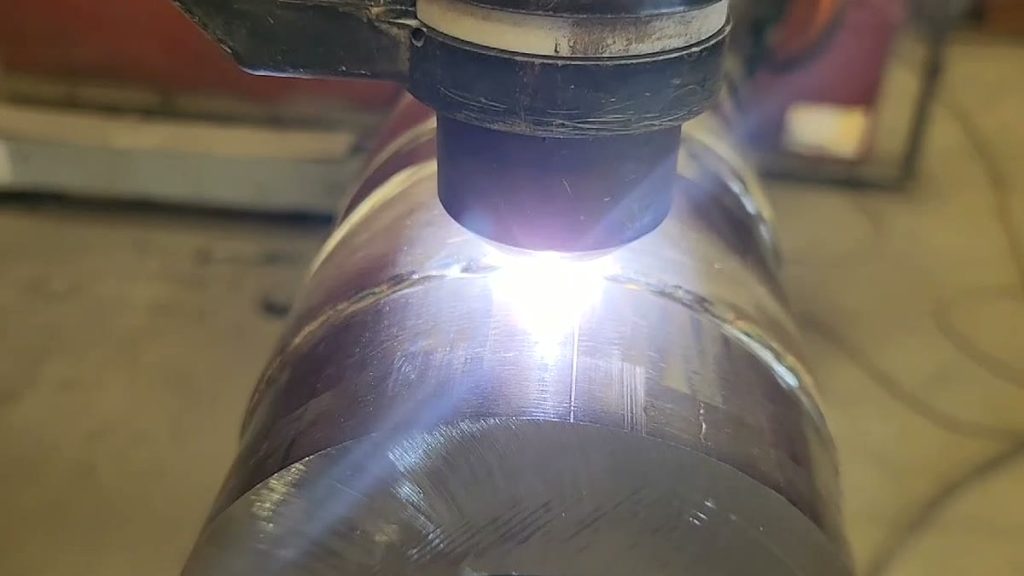
In PTA the pool sits far above the graphitisation temperature, so survival is set by duration: the particle crosses the arc and freezes into the deposit in tens of milliseconds. Titanium coating is the correct specification here, because TiC forms at the interface from about 700 °C and the nickel-based matrix wets that carbide — a chemical bond rather than a grip. The coating is consumed on purpose. It is not a heat shield.
Nickel coating is a different material in the same arc. Nickel melts at 1,455 °C and the nickel–carbon eutectic sits at 1,326 °C, so the film becomes a carbon solvent at the interface instead of a barrier. It belongs in resin and metal bond tools, where the job is a rougher, wettable surface at a few hundred degrees.
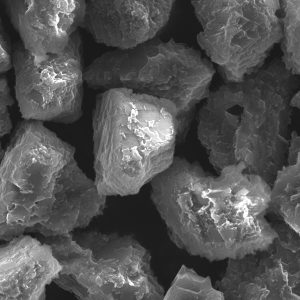
Shape decides pull-out. Crushed grit is angular, interlocks with the matrix as it freezes, then presents micro-cutting edges as abrasive wear moves across the surface. Blocky grit feeds more evenly when diamond is blended into matrix powder at a few percent by weight.
What To Put In The Enquiry
- The route and the matrix alloy, so the thermal cycle is known.
- Size band in µm, with the method used to measure it.
- Coating type and coating weight as a percentage, not a coating grade name.
- Crushed or blocky, and whether fines below the band are screened out.
- Packing, because an oxidised coating bonds to nothing.
Next Step
Send the route, the alloy and the size band, and we will quote a coating weight and a screened cut against it. Trial quantities are available so the powder can be run in your torch before a production order.
Diamond Grades For Each Hardfacing Route
The same mesh behaves differently in the same torch depending on coating, shape and the width of the band. Sizes below are the ranges our hardfacing customers order most.
| Route | Recommended grade | Size band | Why this grade |
|---|---|---|---|
| Diamond enters the arcPTA, laser cladding, spray-fusing | |||
| PTA overlay | Titanium-Coated Diamond | W7 and coarser (band quoted in µm) | TiC forms at the interface inside the arc and the nickel matrix wets it — a chemical bond |
| Laser cladding | Titanium-Coated Diamond | W7 and coarser | Faster cooling shortens the time above graphitisation, so a thinner coating is enough |
| Spray-fused or brazed overlay | MBD High-Strength Diamond Grit | 18/20 – 60/80 mesh | Blocky crystal with controlled impact strength through the brazing cycle |
| Diamond held by the matrixNi-Cr brazing, sintered segments, bond tools | |||
| Ni-Cr brazed hardfacing | HDHR / HDYR Crushed Diamond Grit | 80/100 – 325/400 mesh | Angular facets interlock with the matrix and resist pull-out under impact |
| Resin and metal bond tools | Nickel-Coated Diamond, 30% or 56% | 20/25 – 60/80 mesh | Rougher, wettable surface for the bond. Not a PTA material |
| Fine finishing overlay | HDYP Polycrystalline Diamond Micron Powder | 0.7 – 40 µm | Many cutting edges per particle, renewing as it wears |
Coating weight is quoted as a percentage, not as a grade name. A bead that comes back graphite-grey is a heat-input problem before it is a powder problem — check travel speed and current before changing the diamond.
What has to hold
- Coating intact on arrival — an oxidised film bonds to nothing
- Size band in µm with the measurement method stated
- Crushed or blocky declared, fines below the band screened out
- Coating weight given as a percentage
- Sealed, desiccated packing with a stated shelf life
Where it ships
Diamond Grades For This Process
Factory Direct Since 1990
Zhecheng Hongxiang Superhard Material Co., Ltd. is an integrated manufacturer and exporter of synthetic diamond powders since 1990, located in the Diamond Capital of China.
- Own manufacturing base in Zhengzhou, Henan — powder, coating and grading on one site.
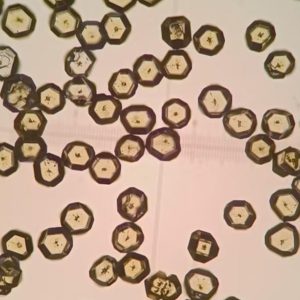
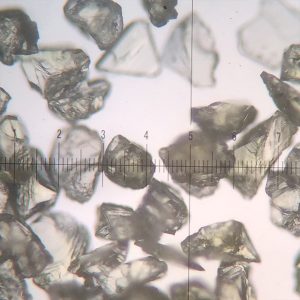
- In-house particle size and SEM inspection on every batch before packing.
- Export packing with neutral or custom label, plus sample quantities for process trials.
What To Include
Describe your workpiece, process and target result. We will match the diamond grade from the existing product range.